Most spare parts forecasts are built from order history: what sold last quarter, last year, the year before. For a manufacturer supporting machines in the field, that history is thin, late and easy to misread. A review by researchers at Erasmus University Rotterdam, Dekker, Pinçe, Zuidwijk and Jalil, states the problem in its first sentence: “Demand for spare parts is often difficult to forecast using historical data only.” Their conclusion is that forecasts “can be made considerably more timely and accurate by using installed base information.”
The installed base is the machines themselves: how many are still in service, where they are, and how hard they are working. It is a different input from anything in the order book, and most manufacturers hold far less of it than they assume.
Key Takeaways
- Spare parts demand is intermittent and erratic, so order history alone produces forecasts that are too thin and too late to plan from.
- The machines in service are the cause of parts demand, which makes their number, location and usage the most useful forecasting input.
- Manufacturers usually lose sight of where machines are and how they run soon after the sale, which is exactly what a parts forecast needs.
- Machines that report their own runtime and location turn the installed base from an estimate into a measured record.
 Order History Is a Thin Signal
The review describes spare parts demand as “usually intermittent, erratic and slow moving,” with the result that “little data is available to perform forecasts based on time series analysis.” A part that sells twice in one quarter and not at all in the next gives a statistical model almost nothing to work with.
The scale of the problem makes it worse. The authors note that servicing an installed base “may require several thousands of distinct parts,” many of them expensive, and many at risk of becoming obsolete before they are used. Safety stock on every item is unaffordable. No stock on a critical item means a customer’s machine stands idle while a part is found.
Lead times add the final complication. Moving a part from a warehouse takes hours or days, but making a new batch of a part can take far longer, which the paper puts at “up to two years” in some cases. A forecast that only reacts to orders after they arrive is always behind the machines it is meant to serve.
The Machines Are the Cause of the Demand
The paper defines the installed base as “the whole set of systems/products a company has sold and which are still in use,” and treats installed base forecasting as “a kind of causal forecasting.” The distinction matters. A time series model looks at past demand and extends the line. A causal model asks why demand happens, and for spare parts the answer is the machines.
Parts demand follows machine sales, with a delay. Early in a product’s life some demand comes from quality problems. Through the rest of its life, demand comes from wear and failure, which depend on how many machines are running and how much they run. Late in the life cycle, demand falls as machines are retired.
Each of those phases is visible in the installed base before it is visible in the order book. The manufacturer that can count its running machines, and see what they are doing, can see the demand coming instead of measuring it after the fact.
Where the Machine Is Decides Where the Part Should Be
Spare parts networks are usually built in tiers, with central stock supplying regional and forward locations closer to customers. The closer the stock, the faster the repair, and the more expensive the network. The review is direct about what that tradeoff depends on: “For a good stocking decision at a forward stock location, it is important to know exactly the installed base for the clients in the neighborhood.”
It is also direct about why that information goes wrong: “Yet the customer may relocate his systems without informing the OEM.” Equipment is moved between sites, sold on, sent to a new project or shipped to another country. The location recorded at the time of sale stops being true, and nobody tells the parts planner.
A forward stock location planned around last year’s machine locations is stocked for the wrong fleet. The right part is in the wrong place, and the cost shows up as emergency shipments, longer downtime and the second service visit that first-time fix rates are meant to prevent.
How Hard a Machine Works Decides How Fast It Wears
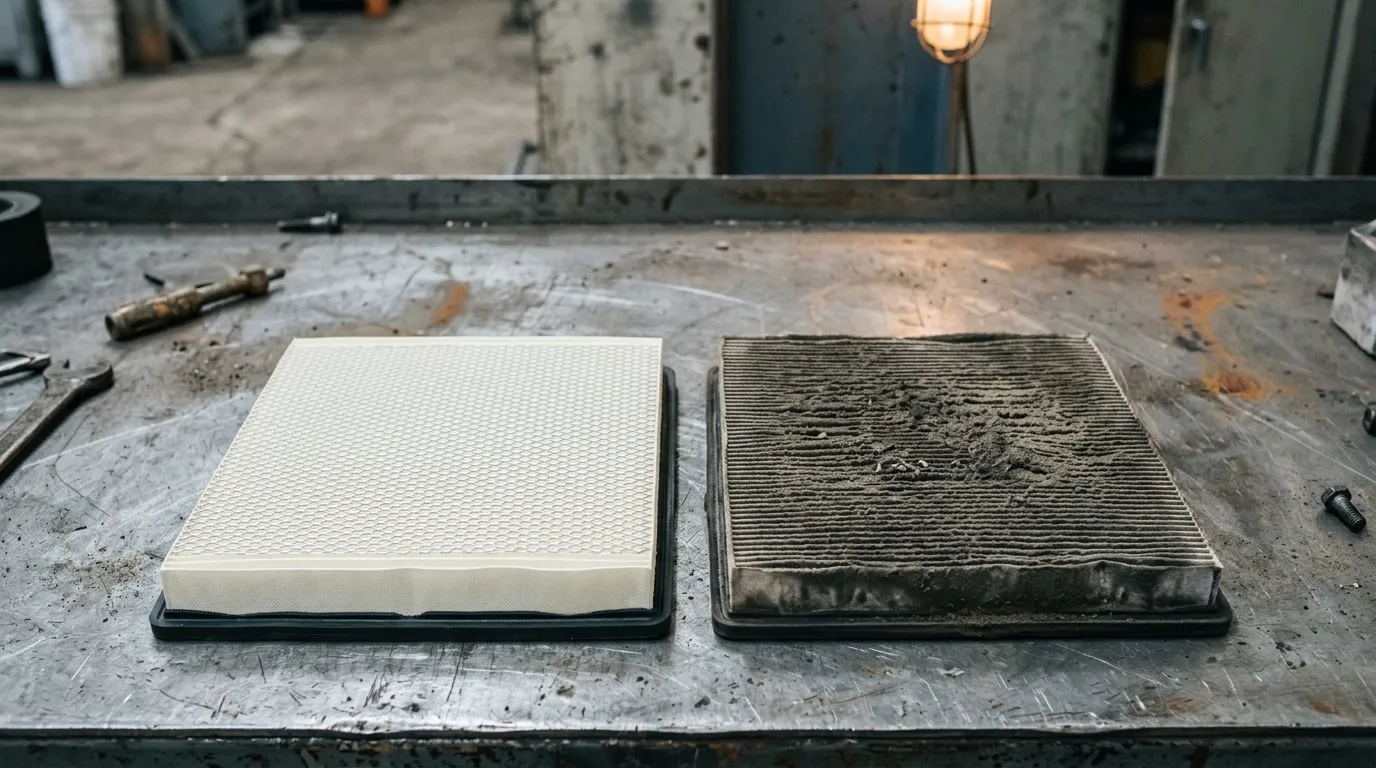 Two machines sold in the same month to two different customers do not need parts at the same time. One runs a single shift a few days a week. The other runs around the clock in heat and dust. The paper gives an aviation example, noting that “most airplane maintenance is fly hour driven,” and a military one: tanks operated in Iraq “needed many more engine filters than the same tanks operated in the United States.”
The same is true of commercial and industrial equipment. Wear tracks hours of use, load and operating conditions far more closely than it tracks the calendar. A forecast that assumes every machine ages at the same rate will be too high for some customers and too low for others, and the errors do not cancel out, because the parts are needed in different places at different times.
Runtime is the single most useful usage figure a manufacturer can have. It is also the one that is usually missing, because it lives on an hour meter on the machine rather than in any system the manufacturer can read.
Seeing the End of Demand Before It Arrives
Spare parts planning does not end when production of a machine stops. The paper notes that the service period after production ends “can be up to decades for some equipment,” and that a manufacturer must estimate demand over that remaining period to size the final production run of a part.
That estimate depends on how many machines are still in service. The review notes that a manufacturer should receive information when a customer abandons a system, and that records for older machines are often scattered across legacy systems. When that information does not arrive, the installed base on paper is larger than the installed base in reality, and the final buy is sized for machines that no longer exist.
The authors also analyse what happens when a drop in demand can be anticipated. Their finding is that when “the time and the size of a drop in demand can be foreseen,” taking it into account in stocking decisions “can lead to significant cost savings.” Seeing machines go quiet in the field is how that drop becomes foreseeable.
Installed Base Data Decays After the Sale
None of this is new to service planners. The difficulty is keeping the data true. The review lists the causes it observed: the sheer size of the installed base, product configurations that change in the field, the variety of products and customers, older records scattered across legacy systems, and the difficulty of collecting data at all.
It also reports a finding worth knowing before investing in better data. In a case at IBM, errors spread evenly across the installed base did not significantly harm the company’s spare parts planning, while errors concentrated in particular areas did. Our reading is that a representative picture of the whole fleet is more valuable than perfect data in one region and none in another. A good installed base record does not need to be flawless. It needs to be consistent.
For a deeper look at why the installed base goes dark after shipment in the first place, see why manufacturers lose track of equipment after it ships.
 Where ARMOR™ Fits
ARMOR™ supplies the two installed base facts a parts forecast depends on and order history cannot provide: where each connected machine is, and how much it has run. ARMOR 4+™ wires into the machine’s electrical system and reports runtime hours, voltage and current into ARMOR Asset Central™, the system of record for runtime, location, condition and activity across the fleet.
ARMOR™ does not forecast parts or run inventory planning. It gives the people and systems that do a measured view of the machines in service, and it sits alongside existing ERP and parts systems rather than replacing them.
The unit installs non-destructively on standard wiring harnesses, with no bill-of-materials redesign. How it is built in at the production stage is set out on the ARMOR™ for Equipment Manufacturers page.
Frequently Asked Questions
Do we need every machine connected before this is useful?
No. The IBM finding in the review suggests that evenly spread gaps matter less than gaps concentrated in one place. A connected share of the fleet that is spread across regions and customer types gives a usable picture of how the whole installed base behaves.
Does this replace our existing forecasting method?
No. The paper describes installed base forecasting as adding information to historic demand, not discarding it. Order history still tells you what customers bought. Installed base data tells you why, and what is likely to come next.
We sell through dealers. Can we still see the installed base?
Often only partly, because location and usage information tends to stay with the dealer. A shared record that the manufacturer, dealer and customer can all read, with the customer’s consent, is the practical way to keep that information from disappearing after the sale.
Can installed base data help with the final buy on an end-of-life part?
Yes. Sizing a final production run means estimating demand for as long as machines stay in service. Knowing how many machines are still running, and how hard, gives that estimate a basis beyond extrapolating past orders.
See how ARMOR™ is built into equipment like yours, at the build stage. ARMOR™ for Equipment Manufacturers